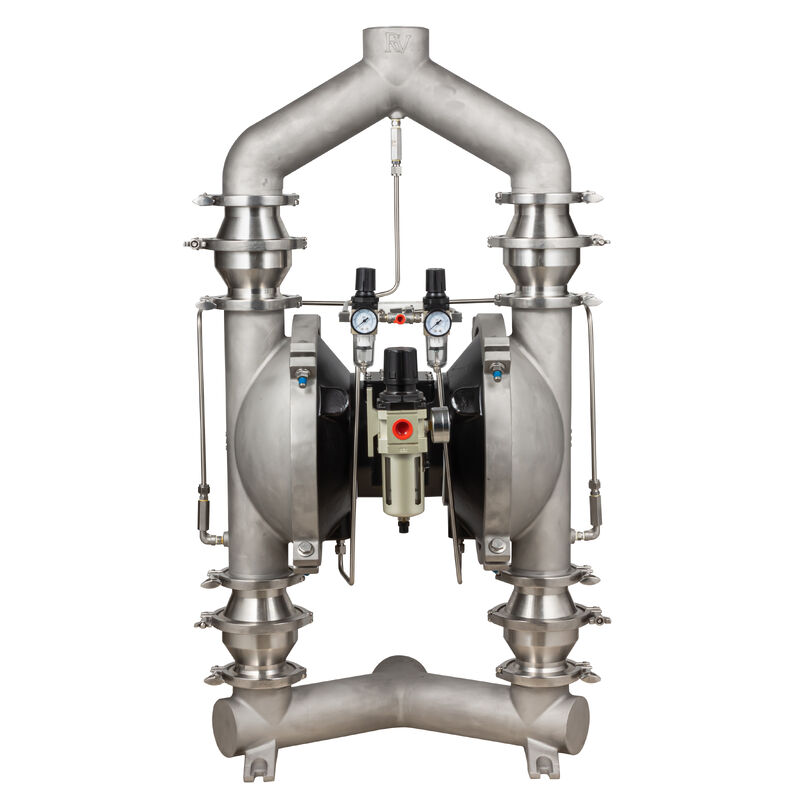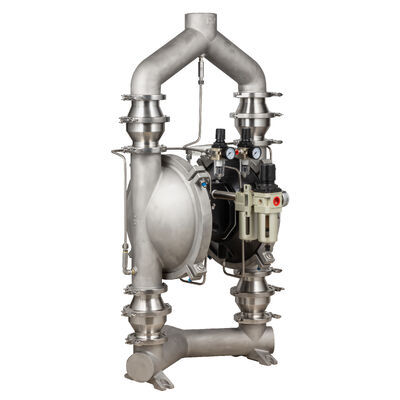
This high-performance Air Operated Diaphragm Pump (AODD is specifically engineered for the safe, efficient, and anti-clogging transfer of dry powders, fine dust, and delicate granules. Built with premium materials and equipped with an integrated air filtration and pressure regulation system, it is the ideal solution for pneumatic powder conveying in chemical, food, pharmaceutical, and industrial manufacturing environments.
Key Features & Benefits for Powder Transfer 100% Dry Running Capability: Unlike centrifugal pumps, this pneumatic pump can run dry without damage, making it perfect for intermittent powder and dust transfer.
Anti-Clogging Design: Features large flow passages and precise valve structures, ensuring smooth handling of fine powders, cement, flour, and chemical dust without blockages.
Integrated Air Treatment System: Comes fully equipped with air filters, regulators, and pressure gauges, ensuring stable operation and preventing moisture from entering the pump chamber.
Superior Safety (Anti-Static & Explosion-Proof): Designed for hazardous environments. The pneumatic drive eliminates electrical sparks, making it highly safe for combustible dust applications. (Optional: Highlight grounding/anti-static features if applicable).
Sanitary & Corrosion-Resistant: Constructed with high-grade stainless steel (e.g., SS316L), providing excellent resistance to corrosion and ensuring the highest hygiene standards for food and pharma applications.
Heavy-Duty Tri-Clamp Connections: Easy to disassemble, clean, and maintain. The secure clamp connections prevent powder leakage during high-pressure transfer.